
Product Short Description
Product Overview
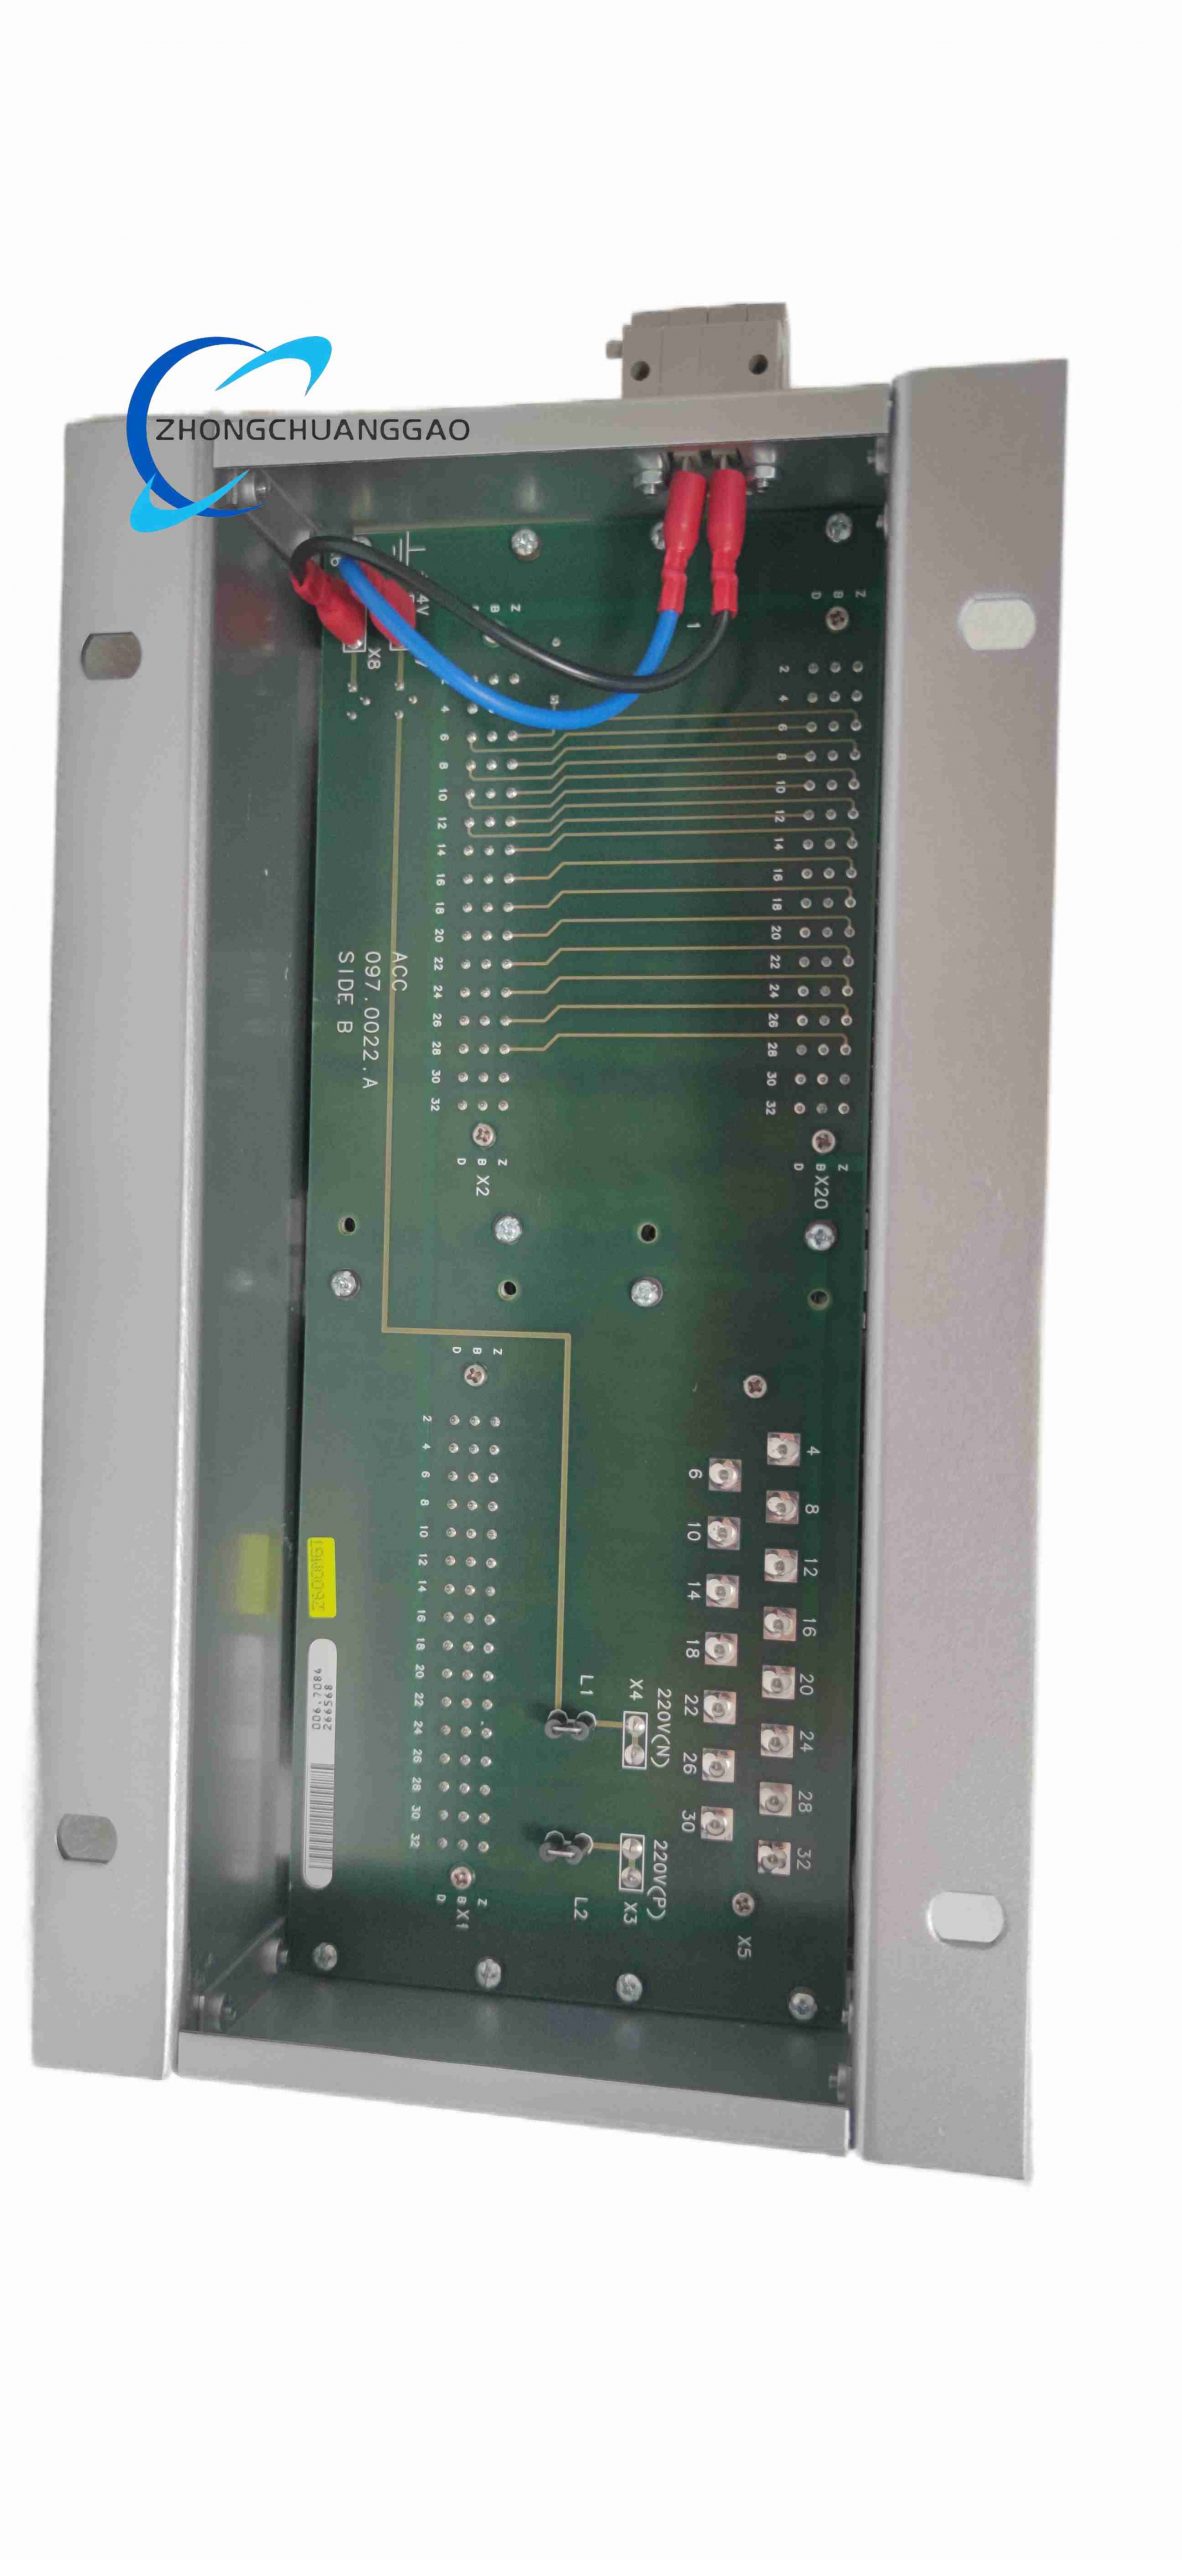
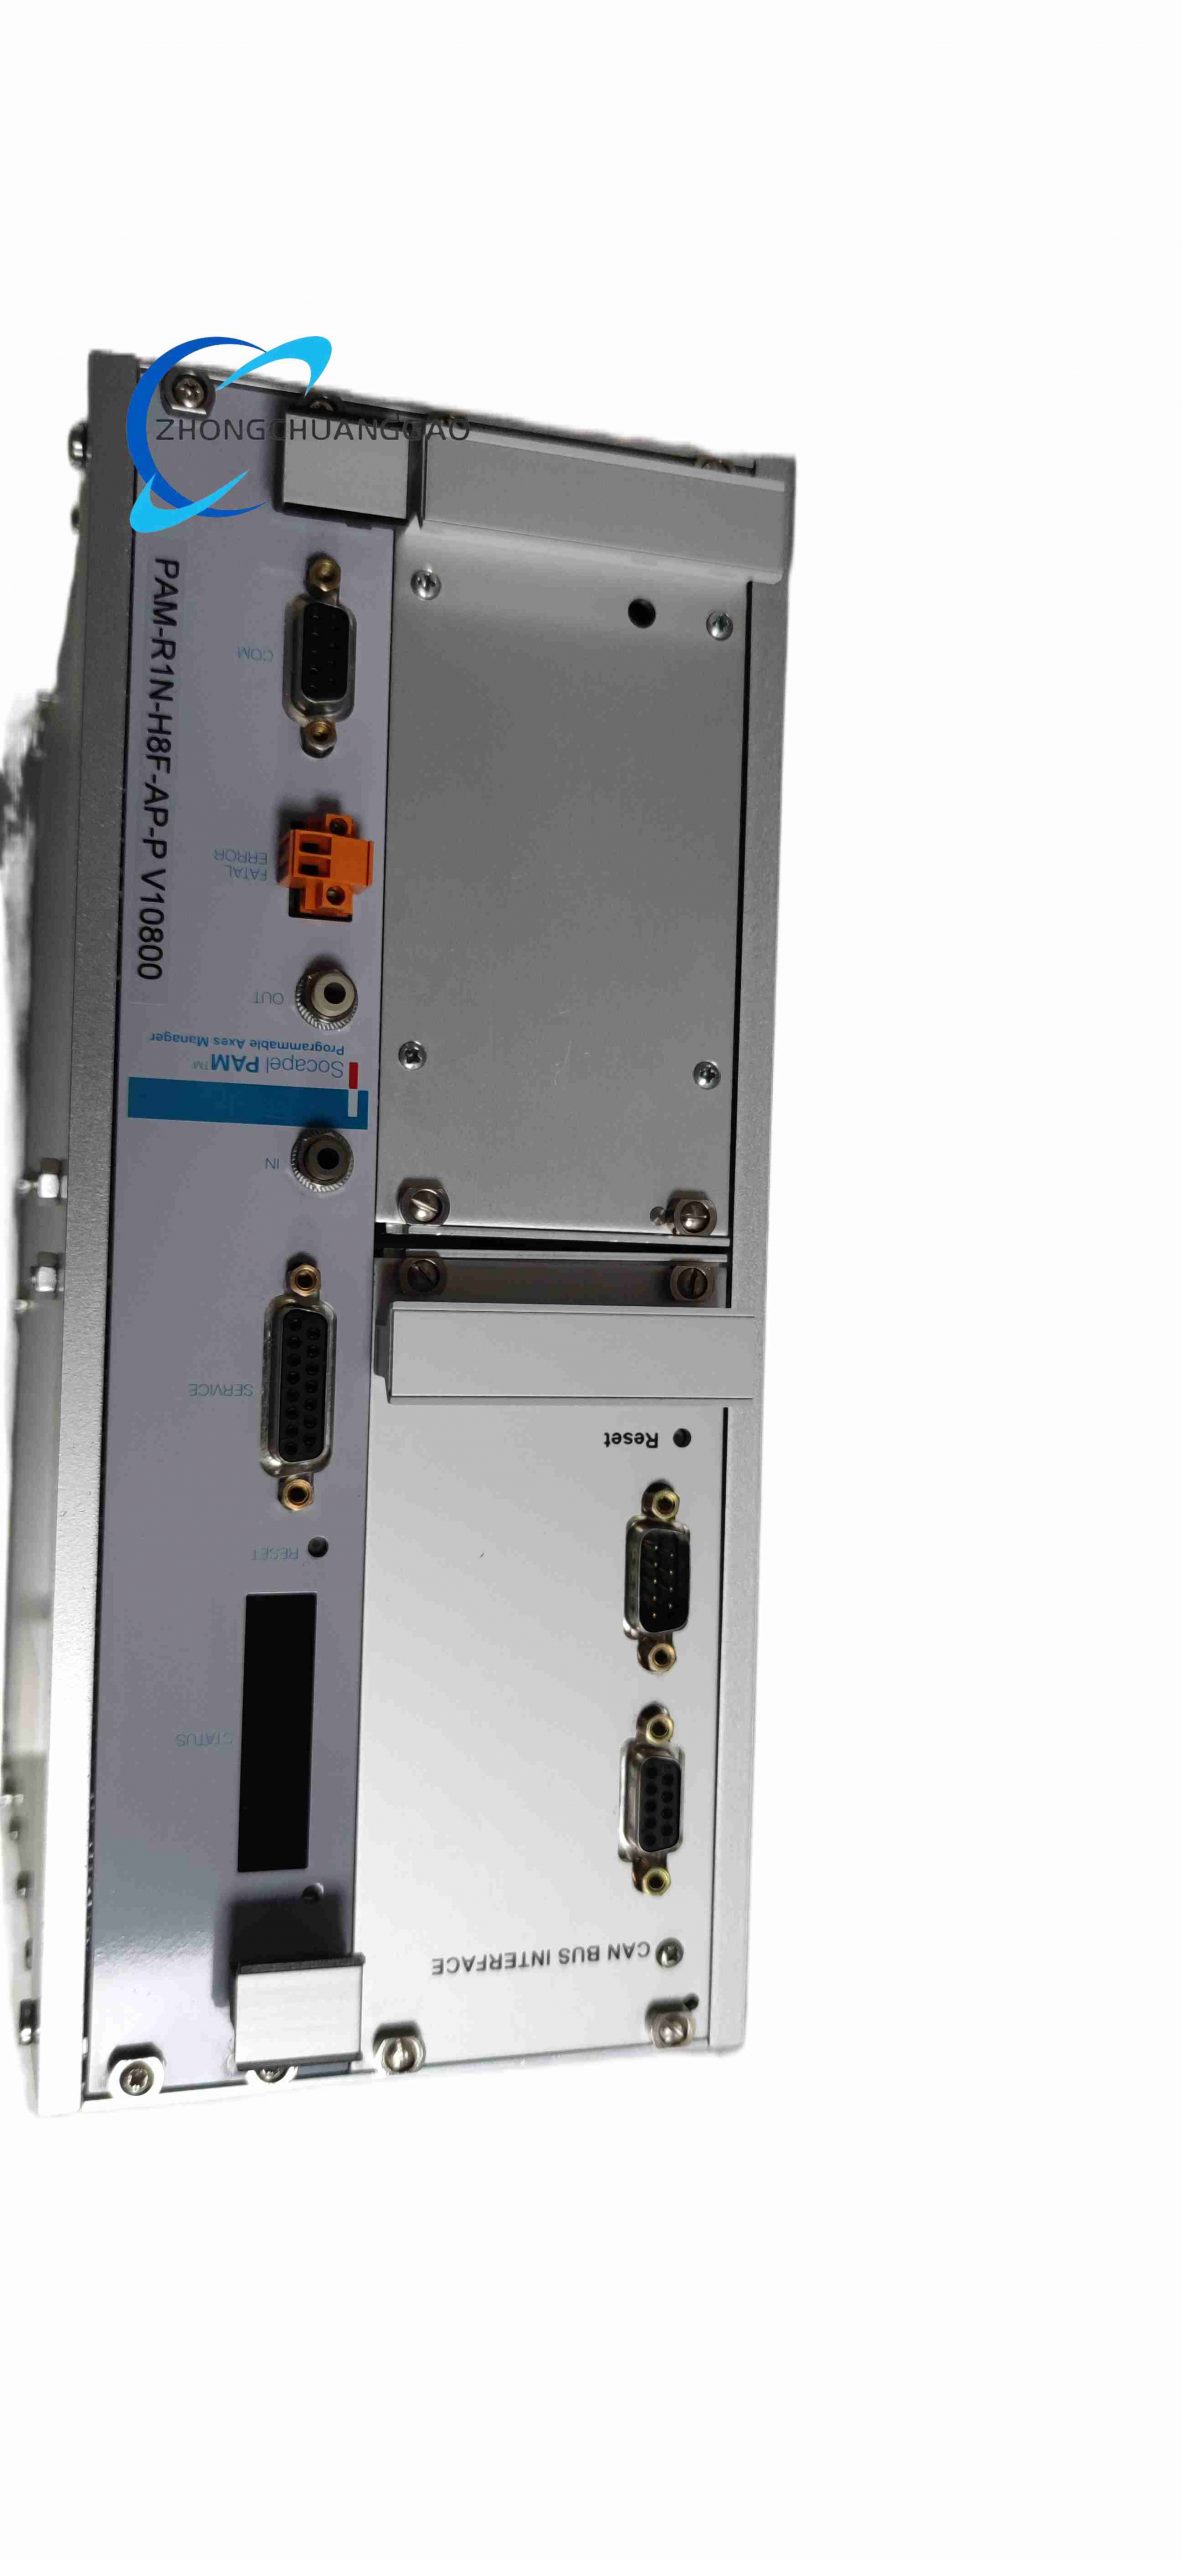
Socapel PAM-R1N-H8F-AP-P V10800 is a distributed high-speed multi-axis synchronization motion control module under H006.7538 part number, dedicated to high-precision printing, textile, and packaging machinery requiring multi-axis electronic cam and phase correction synchronization control. PAM stands for Programmable Axes Manager; V10800 denotes firmware version V10800 with enhanced PAM-Ring fieldbus real-time synchronization performance
Description
Core Technical Specifications
- Power Supply Input: 9–36VDC wide-range industrial DC power; rated power consumption 10W
- Axis Control Capacity: Max 8 synchronized servo axes via proprietary PAM-Ring high-speed fieldbus
- Communication Interfaces: Isolated RS485 Modbus RTU, PAM-Ring dedicated motion bus, digital GPIO expansion channel
- Output Drive Capacity: Analog output max 2A for servo command signal transmission
- Operating Environmental Range: -20°C ~ +85°C; humidity 5–95% RH non-condensing
- Physical Dimension: 140mm(W) × 85mm(H) × 30mm(D); net weight 200g; standard DIN rail mounting
- Firmware Version: V10800 (optimized flying shear, rotary printing press synchronization algorithm)
Function Features
- Distributed multi-axis real-time synchronization with dynamic phase correction during running production speed changes
- Replace mechanical cam and gearbox functions fully via software electronic cam curve programming, flexible recipe switching
- Priority task scheduling architecture: motion axis control executed as highest priority, PLC sequential logic processed as secondary low-priority task to eliminate synchronization delay
- Support on-the-fly indexing, variable speed master-slave tracking, and continuous interpolation across all connected servo axes
- Isolated RS485 communication enables data exchange with third-party PLC, HMI, and production data logging systems
- Non-volatile Flash memory stores up to 32 sets of electronic cam motion recipes for rapid product changeover
- Built-in fault diagnostic function to detect PAM-Ring bus disconnection, servo axis communication loss, and signal short-circuit
Working Principle
- Main master motion speed reference signal (encoder pulse or analog voltage) inputs to PAM module reference channel as master synchronization clock
- Internal high-speed motion DSP calculates electronic cam curve and phase offset for each connected slave servo axis per stored recipe parameters
- Transmit synchronized motion command signals to each servo drive via dedicated PAM-Ring fieldbus with microsecond-level timing precision
- Secondary low-priority task processes digital input/output logic signals for machine auxiliary actuator interlock control
- RS485 Modbus bus uploads real-time axis position, speed, and fault status to upper HMI and production management PLC
- Automatically trigger axis stop interlock and fault code storage upon PAM-Ring bus communication failure or servo drive fault feedback
Material & Structural Characteristics
- DIN Rail Housing: High-temperature resistant black PA plastic with anti-vibration integrated snap mounting clip
- Main Control PCB: Multi-layer isolated circuit board separating high-speed motion bus and low-speed Modbus communication circuits
- Terminal Blocks: Nickel-plated spring-cage screw terminals with wire retention springs for vibration-prone textile/printing workshop environments
- Internal Memory Chip: Industrial grade wide-temperature Flash memory chip to retain motion recipes during power outage
Installation Requirements
- Mount horizontally on 35mm DIN rail inside control cabinet; maintain 20mm vertical clearance between adjacent automation modules
- PAM-Ring motion bus cable uses shielded differential twisted pair, maximum single bus segment length 50m
- Separate motion bus wiring from high-power inverter and servo motor power cables with ≥25cm distance to avoid timing jitter interference
- 24VDC power supply wiring fitted with 1A slow-blow fuse for over-current protection
- Connect module protective earth terminal to cabinet low-resistance grounding bar
Usage Precautions
- Do not modify electronic cam curve parameters during machine running production; pause equipment before recipe editing
- Upgrade firmware version V10800 only via official Socapel configuration software to avoid motion algorithm compatibility failure
- Clean cabinet ventilation filters monthly to prevent dust accumulation leading to module over-temperature shutdown
- Do not daisy-chain more than 8 servo axes on single PAM-Ring bus to maintain synchronization timing accuracy
- Perform full axis synchronization test after replacing any PAM module or servo drive unit before resuming mass production
Reviews
There are no reviews yet.